Description
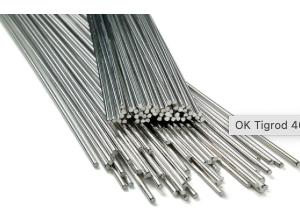
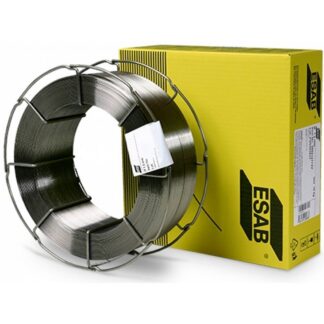
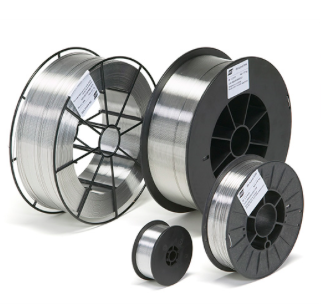
A continuous solid corrosion resisting chromium-nickel wire for welding of austenitic chromium nickel alloys of 18% Cr – 8% Ni-type.
OK Autrod 308LSi has a good general corrosion resistance.
The alloy has a low carbon content making it particularly recommended where there is a risk of intergranular corrosion.
The higher silicon content improves the welding properties, such as wetting. The alloy is widely used in the chemical and food processing industries as well as for pipes, tubes and boilers.
Technical specification
Typical Charpy V-Notch Properties
| Impact Value | Testing Temperature | |||
| As Welded | ||||
| 45 J (33 ft-lb) | -196 degC (-321 degF) | |||
| 70 J (52 ft-lb) | -60 degC (-76 degF) | |||
| 110 J (81 ft-lb) | 20 degC (68 degF) | |||
Typical Tensile Properties
| Condition | As Welded | As Welded |
| Shielding Gas | Tested at 350°C. | |
| Tensile Strength | 570 MPa (83 ksi) | 490 MPa (71 ksi) |
| Yield Strength | 400 MPa (58 ksi) | 370 MPa (54 ksi) |
| Elongation | 36 % | 25 % |
Recommended Welding Parameters
| Wire Diameter | ||||
| 0.6 mm (0.025 in.) | ||||
| 1.14 mm (0.045 in.) | ||||
Deposition Data
| Current | Deposition Rate | Diameter | Voltage | Wire Feed Speed |
| 55-160 A | 1.0-4.1 kg/h (2-9 lb/h) | 0.8 mm (0.030 in.) | 15-24 V | 4.0-17.0 m/min (157-669 in./min) |
| 65-220 A | 1.1-5.4 kg/h (2-11 lb/h) | 0.9 mm (0.035 in.) | 15-28 V | 3.5-18.0 m/min (138-709 in./min) |
| 80-240 A | 1.5-6.0 kg/h (3-13 lb/h) | 1.0 mm (0.040 in.) | 15-28 V | 4.0-16.0 m/min (157-630 in./min) |
| 100-300 A | 1.6-7.5 kg/h (3-16 lb/h) | 1.2 mm (0.047 in.) | 15-29 V | 3.0-14.0 m/min (118-551 in./min) |
| 230-375 A | 5.2-8.6 kg/h (11-19 lb/h) | 1.6 mm (1/16 in.) | 23-29 V | 5.5-9.0 m/min (217-354 in./min) |
Classifications
| Wire Electrode | SFA/AWS A5.9 : ER308LSi Werkstoffnummer : ~1.4316 EN ISO 14343-A : G 19 9 L Si |
Approvals
| Approvals | BV 308L SA BT (M12) CE EN 13479 CWB ER308LSi DB 43.039.01 DNV-GL VL 308 L (M13) NAKS/HAKC 0.8-1.2 mm VdTÜV 04267 |
| Approvals are based on factory location. Please contact ESAB for more information. |
Consumable Characteristics
| Alloy Type | Austenitic (with approx. 8 % ferrite) 19% Cr – 9% Ni – Low C – High Si |
Typical Weld Metal Analysis %
| Typical Wire Composition % | ||||||||||||||
| C | Cr | Cu | Mn | Mo | Ni | P | S | Si | Si+Fe | |||||
| 0.01 % | 19.9 % | 0.10 % | 1.8 % | 0.15 % | 10.5 % | – | – | 0.9 % | 9 % | |||||
| Typical Weld Metal Analysis % | ||||||||||||||
| 0.01 % | 20 % | 0.1 % | 1.8 % | 0.1 % | 10 % | 0.015 % | 0.015 % | 0.8 % | – | |||||