Description
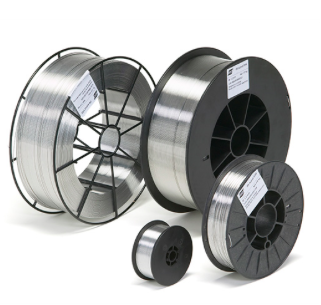
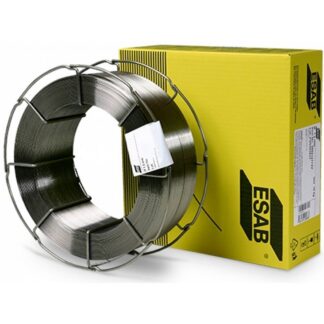
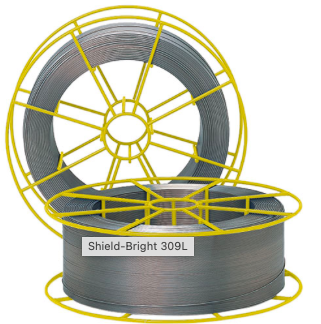
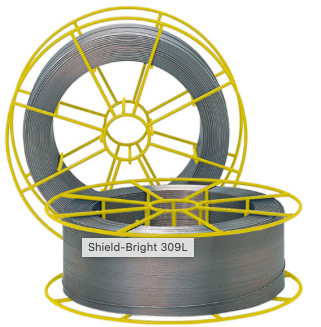
Shield-Bright 2209 was developed for the welding of “2205” duplex stainless steels (UNS S31803, S32205, and J92205).
It can also be used for the welding of leaner grades of duplex stainless steels.
It has been approved with a 25°C critical pitting temperature and impact toughness at -40°C (-40°F).
Technical specification
Typical Charpy V-Notch Properties
| Impact Value | Testing Temperature | |||
| As Welded 80%Ar/20%Co2 Shielding Gas (M21) | ||||
| 52 J (38 ft-lb) | -46 degC (-51 degF) | |||
| As Welded Co2 Shielding Gas (C1) | ||||
| 50 J (37 ft-lb) | -46 degC (-51 degF) | |||
Typical Tensile Properties
| Condition | As Welded | As Welded |
| Shielding Gas | 80%Ar/20%CO2 Shielding Gas (M21) | CO2 Shielding Gas (C1) |
| Tensile Strength | 810 MPa (117 ksi) | 800 MPa (116 ksi) |
| Yield Strength | 670 MPa (97 ksi) | 650 MPa (94 ksi) |
| Elongation | 28 % | 28 % |
Deposition Data
| Current | Deposition Rate | Diameter | Voltage | Wire Feed Speed |
| 130-220 A | 1.9-4.6 kg/h (4-10 lb/h) | 1.2 mm (0.045 in.) | 25-30 V | 5.8-14.4 m/min (228-567 in./min) |
| 170-300 A | 2.4-5.2 kg/h (5-11 lb/h) | 1.6 mm (1/16 in.) | 25-29 V | 3.9-8.2 m/min (154-323 in./min) |
Classifications
| Weld Metal | SFA/AWS A5.22 : E2209T1-4, E2209T1-1 EN ISO 17633-A : T 22 9 3 N L P C1 2 EN ISO 17633-A : T 22 9 3 N L P M21 2 |
Approvals
| Approvals | ABS E2209T1-1 ABS E2209T1-4 BV 2205 (C1) BV SA 2205 CCS 2205-S (C1) CE EN 13479 CWB E2209T1-1 (C1) CWB E2209T1-4 (M21) DNV Duplex (C1) DNV-GL Duplex (M21) LR S31803 S (C1, M21) RINA 2209 S VdTÜV 09123 |
| Approvals are based on factory location. Please contact ESAB for more information. |
Consumable Characteristics
| Alloy Type | Ni, Cr, Mo, N |
| Welding Current | DC+ |
Typical Weld Metal Analysis %
| Typical Weld Metal Analysis % | ||||||||||||||
| C | Cr | Mn | Mo | N | Ni | P | S | Si | Si+Fe | |||||
| C1 | ||||||||||||||
| 0.03 % | 23.2 % | 1.40 % | 3.21 % | 0.14 % | 8.7 % | 0.025 % | 0.012 % | 0.60 % | 40 % | |||||
| M21 | ||||||||||||||
| 0.03 % | 22.5 % | 0.90 % | 3.2 % | 0.16 % | 9.2 % | 0.025 % | 0.012 % | 0.35 % | 40 % | |||||