Description
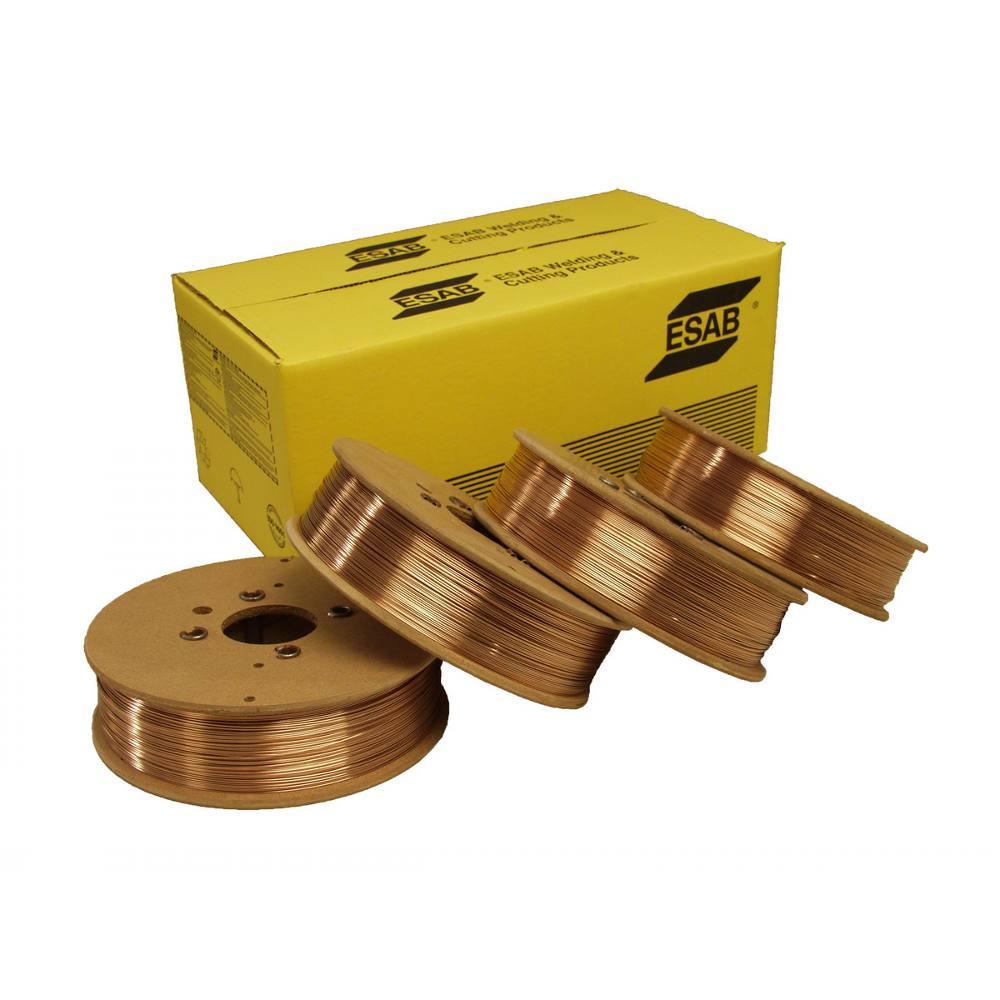
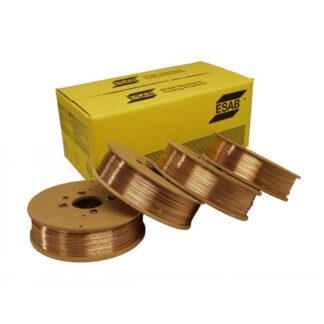
A copper coated, G3Si1 solid wire for GMAW of all general structural and engineering unalloyed and low-alloyed carbon-manganese steels.
The electrode may be welded with either a gas mixture or with pure CO2 as the shielding gas.
Technical specification
Typical Tensile Properties
| Condition |
As Welded |
As Welded |
|
|
|
|
|
|
|
|
|
|
|
|
|
|
|
| Shielding Gas |
EN 80Ar/20CO2 (M21) |
EN CO2 (C1) |
| Tensile Strength |
560 MPa |
|
| Yield Strength |
470 MPa |
|
| Elongation |
26 % |
|
|
|
Deposition Data
| Current |
Deposition Rate |
Diameter |
Voltage |
Wire Feed Speed |
| 0.0-0.0 kg/h |
– |
1.6 mm |
– |
– |
– |
0.0-0.0 m/min |
| 60-180 A |
0.8-2.6 kg/h |
– |
0.8 mm |
– |
– |
– |
18-22 V |
0.8-2.6 m/min |
| 80-250 A |
1.0-4.8 kg/h |
– |
1.0 mm |
– |
– |
– |
18-30 V |
1.0-4.8 m/min |
| 120-330 A |
1.3-6.9 kg/h |
– |
1.2 mm |
– |
– |
– |
18-34 V |
1.3-6.9 m/min |
Classifications
| Wire Electrode |
EN ISO 14341-A : G 3Si1
SFA/AWS A5.18 : ER70S-6 |
| Weld Metal |
EN ISO 14341-A : G 38 2 C1 3Si1
EN ISO 14341-A : G 42 3 M21 3Si1 |
Approvals
| Grade |
EN 13479 |
| Society |
CE |
| Approvals are based on factory location. Please contact ESAB for more information. |
Consumable Characteristics
| Alloy Type |
Carbon-manganese steel (Mn/Si-alloyed) |
Typical Weld Metal Analysis %
| Wire Composition |
| C |
Mn |
Si |
| 0.078 % |
1.46 % |
0.85 % |