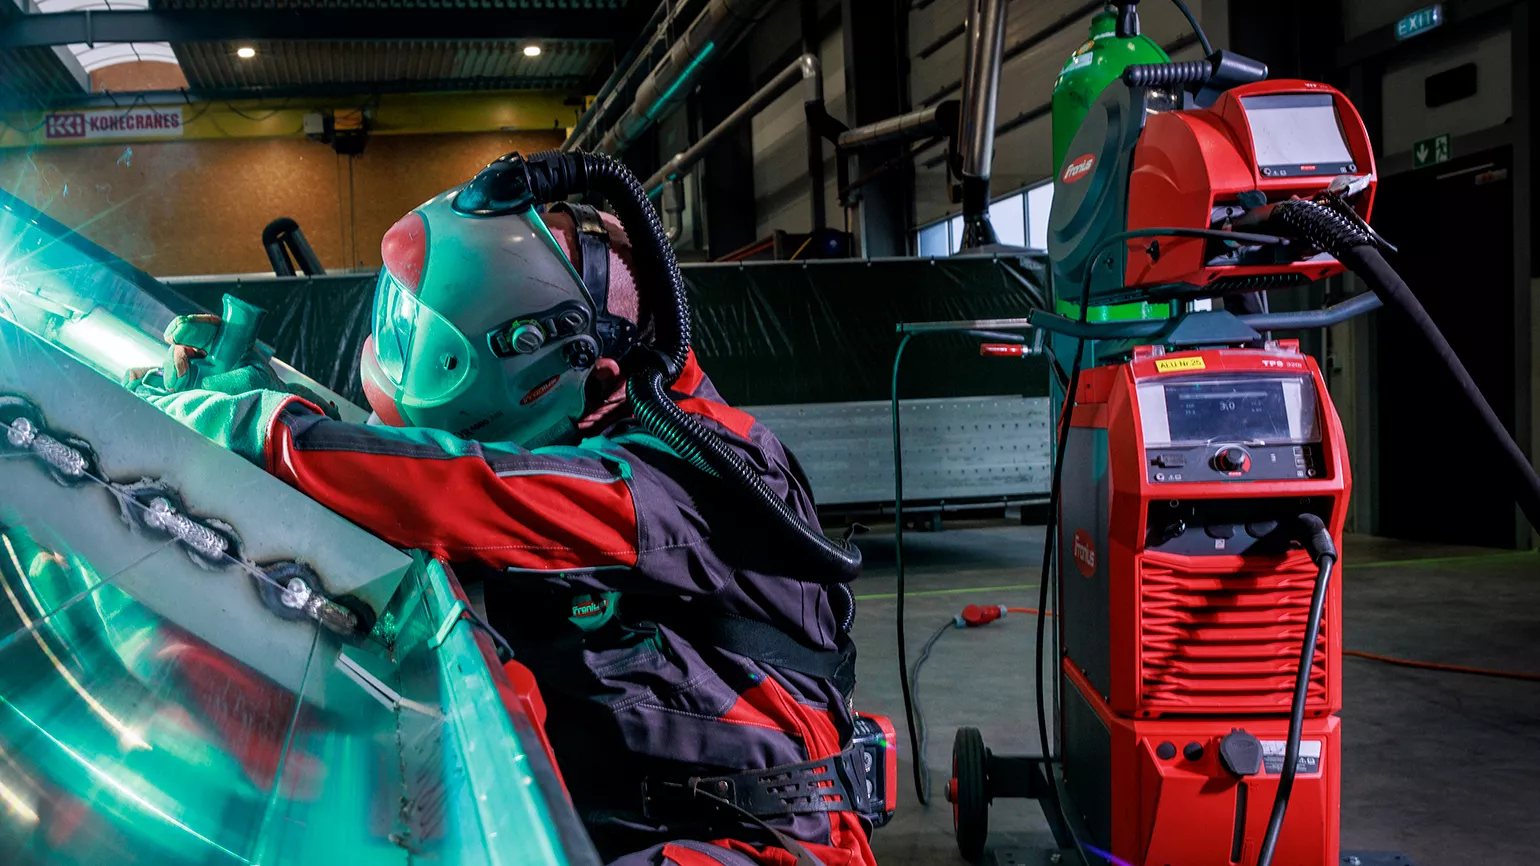
For appearance, TIG has always been the benchmark on aluminium: the evenly rippled “stack of coins” bead that customers love. The trouble is that TIG is slow. Pulse MIG closes much of that gap, giving a well-defined, consistent bead at MIG travel speeds.
Why aluminium is awkward with conventional MIG
- Aluminium conducts heat away very quickly, so it needs plenty of energy to start fusing, then is easy to overheat once it gets going.
- Short-arc MIG on aluminium is prone to lack of fusion, and a conventional spray arc is often too hot for thinner sections.
- Soft aluminium wire is easily crushed or tangled, and thin wires are the worst for feeding problems.
How pulse helps
Pulse MIG delivers spray-type, one-droplet-per-pulse transfer at a lower average current (see What is pulse welding?). On aluminium that means:
- Superb bead definition: an even, rippled bead with very little spatter.
- Good fusion without overheating: the peak current gives penetration, and the background lets the pool settle.
- Thicker wire on thinner material: because the mean current is lower, you can often run a stiffer 1.0 or 1.2 mm wire on sections where you would otherwise need a thin, hard-to-feed wire.
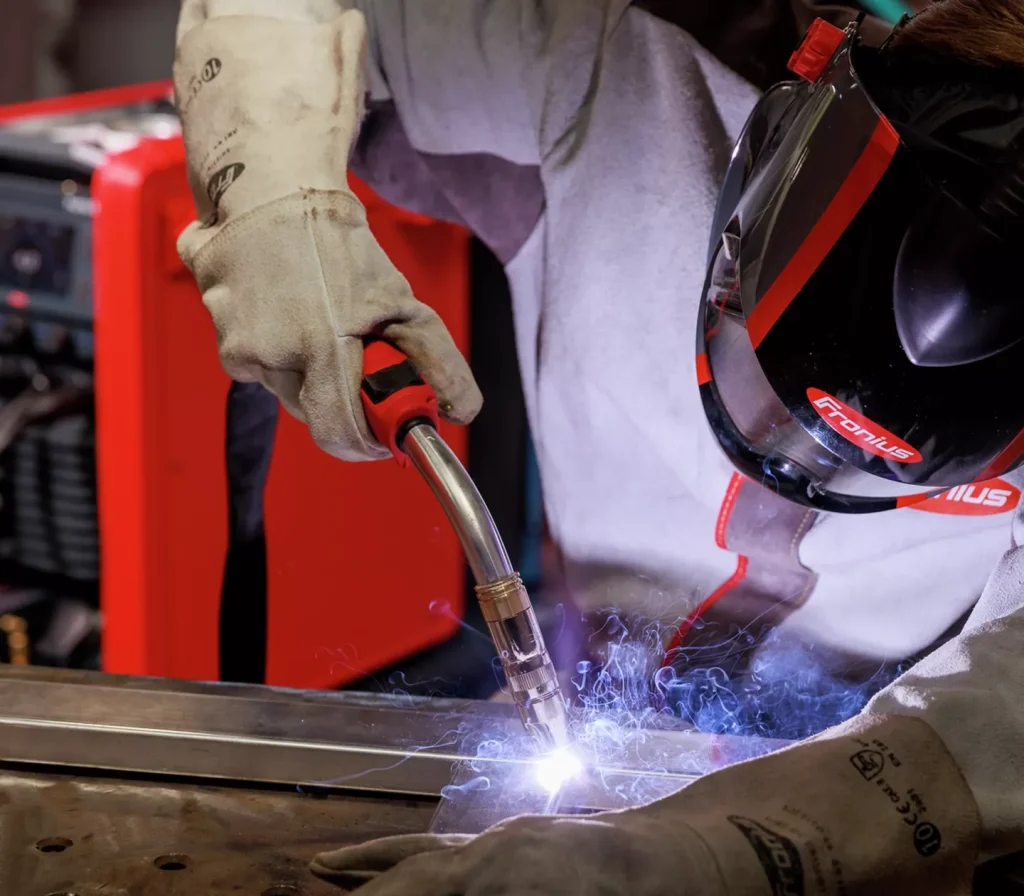
Some machines go a step further. The Fronius Fortis offers SynchroPulse as an extra for aluminium, which varies the power at a low frequency on top of the normal pulse to produce a ripple pattern closer to a TIG weld.
Set-up tips for aluminium
- Use pure argon unless your procedure says otherwise.
- Fit a plastic (PTFE or carbon) liner and U-groove drive rolls, and keep the torch lead as straight as you can.
- Remove the oxide film with a dedicated stainless steel brush, and degrease the joint first.
- Push the torch rather than drag it.
- Pick the right wire for the alloy: 5356 for strength and anodising colour match on most 5000 and 6000 series work, 4043 for better flow and crack resistance, especially on castings. Browse all MIG wire.
For aluminium and stainless steel we recommend a Pulse Welding Package, such as the Fortis 270 C Pulse or Fortis 320 C Pulse.
Talk to us
Tell us the alloy and thickness you work with and we’ll recommend a machine, wire and torch set-up. Call 0141 959 5666 or email info@weldsafe.co.uk.
Images © Fronius International GmbH.